Product: HandySCAN Industry: Consumer Products and Retail
Flatz GmbH from Lauterach, Austria, is the market leader for system solutions in the packaging sector and produces corrugated board, insulating solutions, EPP moldings, and pull containers.
For its quality control workflows, Flatz faced the challenge of having to accurately measure increasingly complex contours of technical components, particle foams, and tools. The surfaces can be matte to glossy, with part sizes ranging from 100 mm to 2500 mm. Therefore, the company decided to acquire modern measurement technology to meet a complete range of quality control requirements.
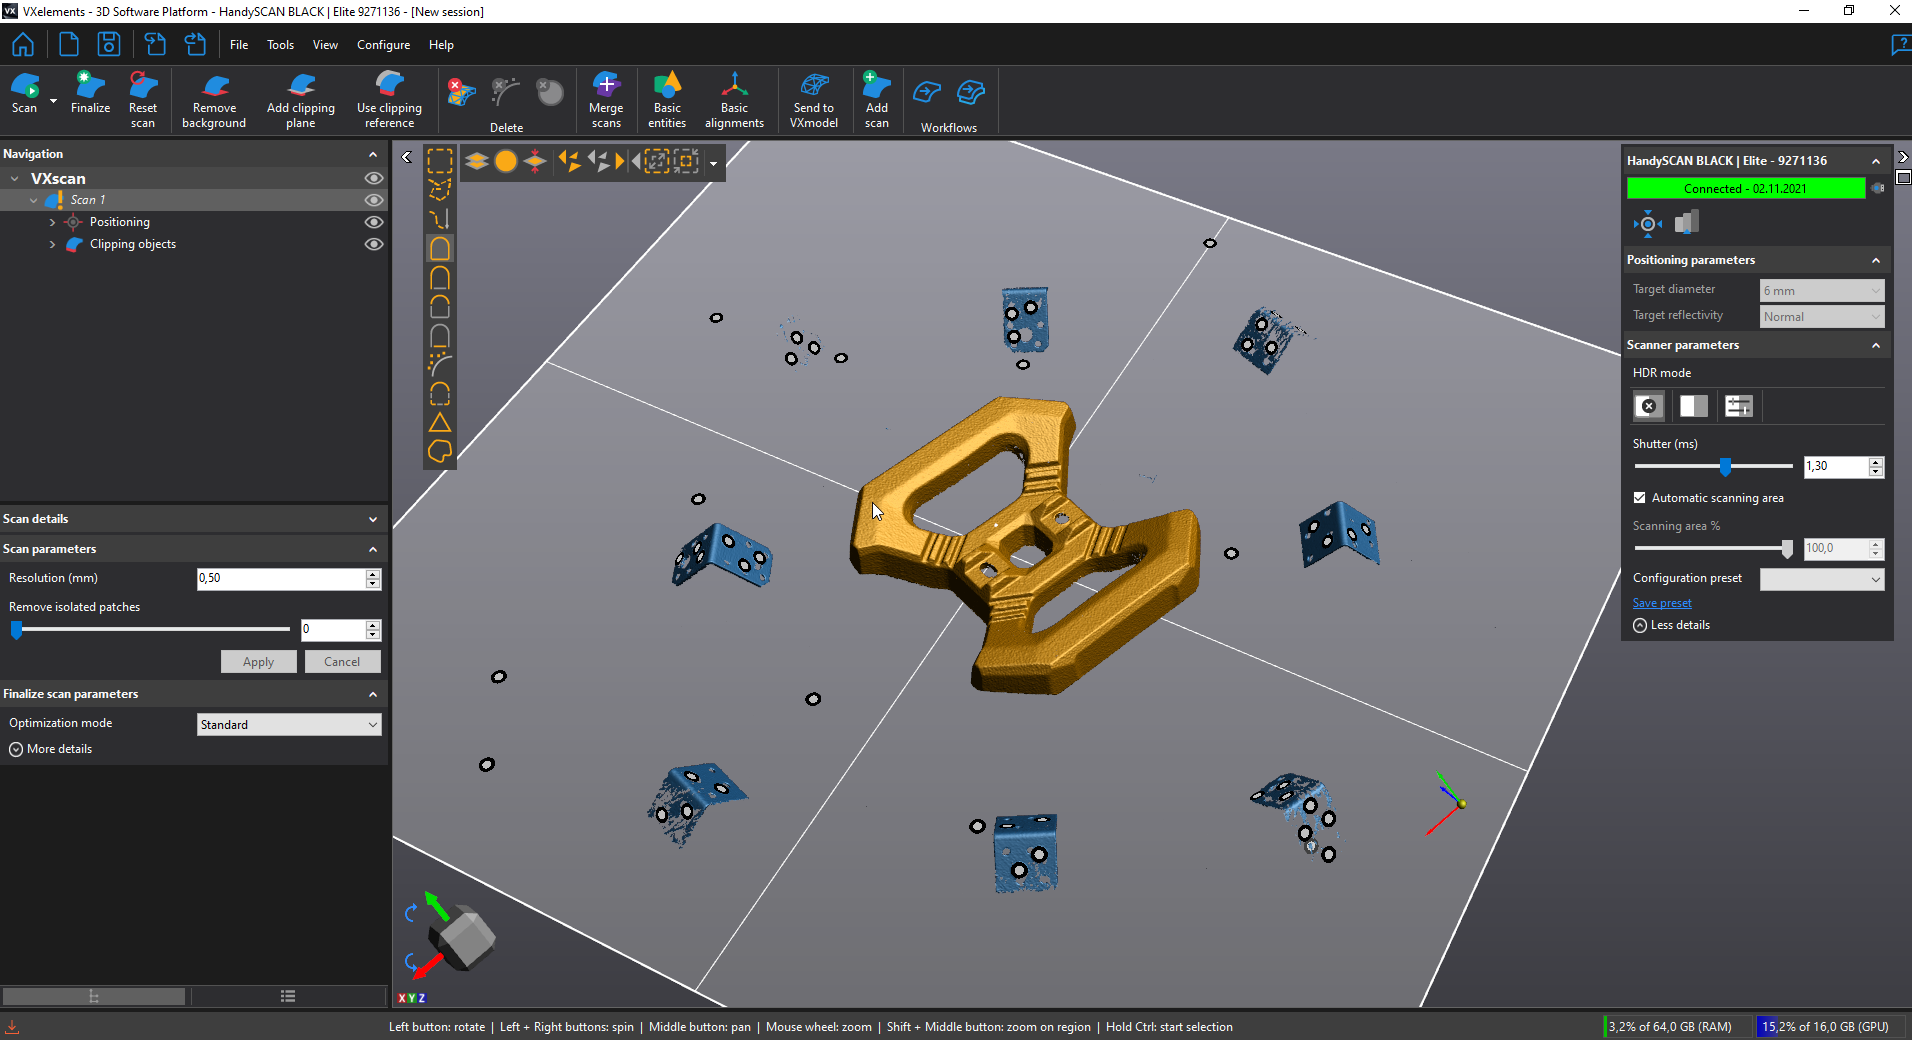
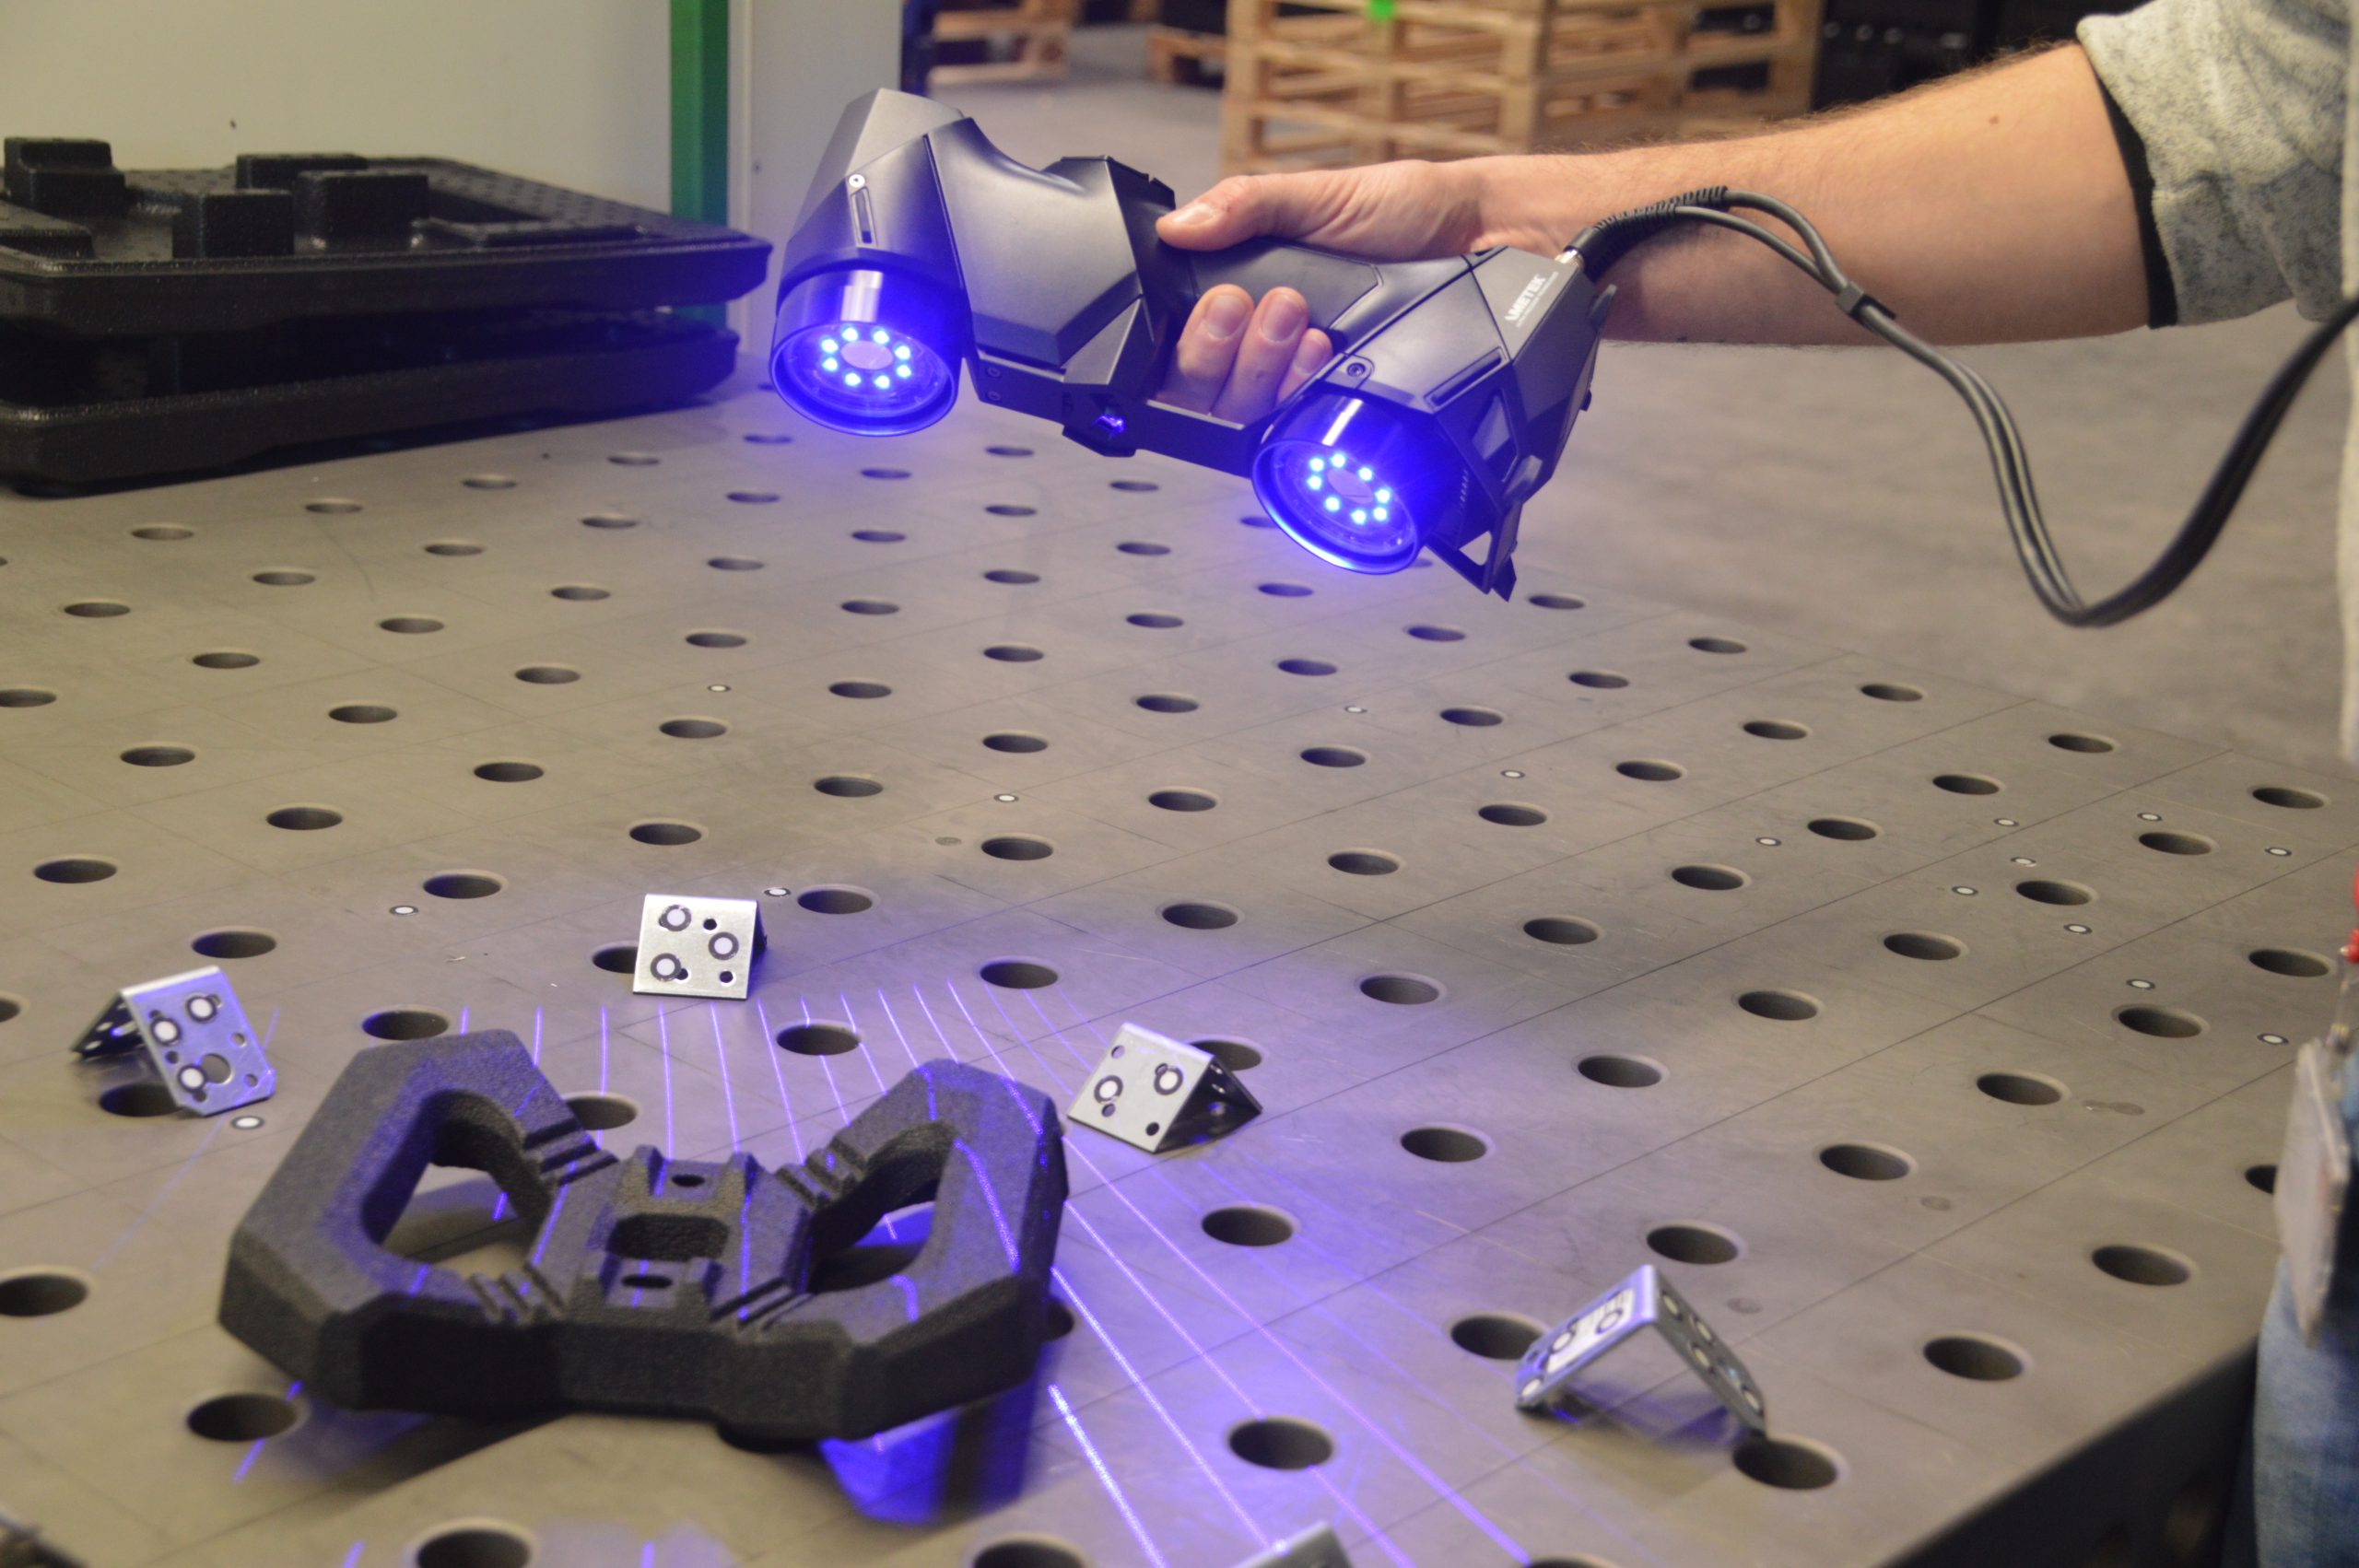
The HandySCAN BLACK Elite from Creaform was the perfect solution. This portable 3D scanner can be used flexibly with an accuracy of 0.025 mm. It can also quickly and accurately measure components of any size, with matte to glossy surfaces in real time. Prior to acquiring Creaform’s new measurement system, Flatz used tape measures, calipers, U-bolts, and similar tools to take measurements.
Bernhard Guldenschuh from Quality Management remarked: “We received excellent training from Creaform, which directly addressed our measurement requirements. We were able to quickly put together a team that can now take measurements on a wide variety of components at any time, if required. Product approvals can now be carried out without any problems.”
EEP part approval
Flatz GmbH had received an order to produce an expanded polypropylene (EPP) part with a size of approximately 250×300 mm for a new customer. It was to be installed on an injection-molded part. EPP is a thermoplastic material that is particularly environmentally friendly and easy to recycle.
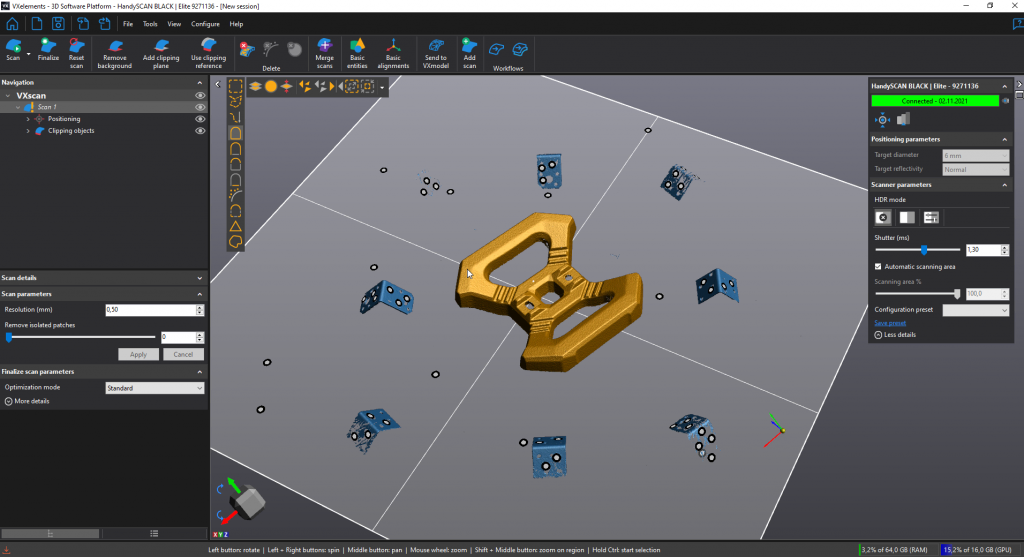
The finished EPP part was mounted on an injection-molded part, which was then to be built into a complex device. The EPP part was designed to protect the interior of the injection-molded component. After sampling, however, there were problems with the fitting accuracy of the part. The customer was unable to install the part. The EPP part produced was scanned with the HandySCAN 3D and compared against CAD data in PolyWorks. It quickly became clear that the injection molded part had the wrong dimensions. It was subsequently adjusted and the EPP part could be installed.
Areas of application for the HandySCAN BLACK at Flatz
The HandySCAN 3D has become an integral part of the sampling and approval process of components at Flatz. It is used for technical component assessments, inspection of complex tooling, and checking dimensional accuracy. It can be used to quickly verify that a part fits, and provide results on part accuracy.
Product: ArtecLeo Industry: Consumer Products and Retail
In the world of custom luxury furniture, clients expect to see what they’re about to order, especially when a virtually unlimited number of combinations of fabrics, leathers, finishes, colors, hardware, and accessories can dramatically change the look and feel of any upholstery or casegoods furniture piece. If not in person, then at least in a printed catalog or online.
But with the traditional method of using photography to create images for product listings, this is no easy feat.
Pairing 3D-scanned custom furniture in a CGI-rendered room scene. (Photo: Sherrill Furniture)
Each individually customized piece must first be manufactured and then captured from multiple angles in a dedicated photo shoot, otherwise the client is simply told to “imagine” what their new furniture will look like when it gets delivered. And from a customer’s point of view, it’s a risky thing to be such a pioneer.
Only the best
For Sherrill Furniture of Hickory, North Carolina, this wasn’t good enough. Ever since opening their doors in 1945, their goal has been maximum customer satisfaction, not just in terms of the highest-quality materials and craftsmanship, but also meeting and exceeding their clients’ expectations every step of the way.
3D-scanned Sherrill Furniture custom chair in a CGI-rendered living room scene. (Photo: Sherrill Furniture)
As such, they searched for a way to show their clients worldwide exactly what the furniture of their dreams was going to look like, even before it’s ever made. And with thousands of unique pieces available, plus dozens of custom furniture programs from across the company’s nine brands, whatever solution they adopted would also need to be fast and flexible.
Sherrill Furniture VP of Marketing Dax Allen and his team’s research led them to 3D scanning as part of a dedicated scan-to-CGI imaging pipeline, one that would allow them to create dozens of fully customizable 3D models for product listings week after week, year in, year out.
3D-scanned Sherrill Furniture custom chairs in a CGI-rendered room scene. (Photo: Sherrill Furniture)
At the same time, this would also streamline their content creation workflow, removing any existing bottlenecks while preventing new ones from ever arising.
With these requirements in mind, they contacted the 3D scanning experts at Artec Ambassador Digitize Designs and spoke with Sales Engineer Bo Helmrich, who immediately recommended the Artec Leo to them.
A fully portable, handheld 3D scanner with a built-in touchscreen and computer, which delivers submillimeter-precise color 3D scans, the Artec Leo excels at capturing medium-sized objects, particularly in places where maneuverability is a must, such as the crowded showrooms where Sherrill Furniture’s design team needs to scan.
“Once I realized how quickly Leo captures data, I started moving faster, and Leo has no problem keeping up with me.”
Handheld, hi-tech solutions
After purchasing their Leo, Allen and his team worked closely with Helmrich in coming up with an efficient workflow for capturing furniture pieces and processing the scans in Artec Studio software.
Sherrill Furniture’s Noah Carney scanning a chair with Artec Leo. (Photo: Sherrill Furniture)
In the words of Design Engineer Tanner Pittmon, “Bo helped me work out the best way to scan whatever kinds of pieces I need to capture, from small chairs all the way up to full-sized sectionals, which means working from left to right, while capturing some of the upper and lower parts of the piece along the way.”
He continued, “With Leo, we don’t need to use any targets or markers at all, and the only problem I had initially was that I was scanning too slowly and too much data was building up. Once I realized how quickly Leo captures data, I started moving faster, and Leo has no problem keeping up with me.”
Original Sherrill Furniture wood-frame chairs awaiting 3D scanning with Artec Leo. (Photo: Sherrill Furniture)
If there’s ever some aspect or detail that wasn’t captured in its entirety, “I can confirm this right away on Leo’s touchscreen while I’m scanning,” Pittmon said, adding, “And then with one wave of the scanner, that’s it, I have everything.”
“Having Leo means never having to return to the showroom for a repeat scan.”
Leo’s ability to make gap-free scans of even complex, naturally shaped furniture is crucial to the workflow. If there were any gaps in the scans when the CGI team receives them, they wouldn’t be able to realistically wrap the virtual upholstery to the model, and the quality would suffer.
That’s one reason why each individual component is scanned separately, and then brought together in Artec Studio later on before sending them to the CGI team. This means every cushion and pillow and other element is scanned by itself, thus ensuring full 360-degree coverage from top to bottom.
Marketing Coordinator Noah Carney said, “With Leo, we don’t have to wait until we’re starting to process the scans to understand whether we missed some detail that’s important for the CGI team to do their work.”
Artec Studio screenshot of the wood-frame chair scan. (Photo: Sherrill Furniture)
Carney explained, “When we visit our showroom, we’ll be capturing 20 pieces or more in one afternoon, and then we’ll head back to the office for processing the scans. Having Leo means never having to return to the showroom for a repeat scan.”
CGI render of the wood-frame chair with customized visualization. (Photo: Sherrill Furniture)
A customized craft
Once the scans are uploaded in Artec Studio software, they’re processed and turned into 3D models, which takes just a few minutes of aligning the various scans for each piece, and cleaning up any non-essential data present.
Processing Leo scans of a chair in Artec Studio software. (Photo: Sherrill Furniture)
Following this, the 3D models are sent over to the CGI team, who import them into ZBrush. There, they focus on refining the geometry in preparation for the next step, which takes place in 3D Studio Max. That’s the stage where they add in seams and UV and other model changes not done in ZBrush.
CGI render of Sherrill Furniture’s Dundee Natural chair, from Artec Leo scans. (Photo: Sherrill Furniture)
The final results of their work are vividly lifelike 3D models of each piece, which can be zoomed in on, inspected up close, and modified at the click of the mouse to change the upholstery from Acapella Red to Zussman Seafoam green, or anything in between.
CGI render of Sherrill Furniture’s Sauvage Saddle chair, from Artec Leo scans. (Photo: Sherrill Furniture)
And various finishes, color schemes, and accessories can be instantly selected and visualized, showing the client exactly what the company’s master craftsmen will be bringing to life and shipping out in the days ahead.
CGI render of Sherrill Furniture custom sofa, from Artec Leo scans. (Photo: Sherrill Furniture)
Pittmon said, “One little trick that we do with Leo for keeping the realism high is when we’re scanning a sofa, for example, we’ll scan both the right and left sides. Many companies out there will take a shortcut and just mirror one side to the other, but we never do that.”
Artec Studio screenshot showing Leo scans of Sherrill Furniture custom sofa set. (Photo: Sherrill Furniture)
He continued, “Because in bench made furniture there are tiny, unique differences between the two sides that will register when you look closely: wrinkles, folds, even the way the light plays upon the surface of the fabric, and without this realism, the model will just look fake.”
CGI render of the same custom sofa set, visualized with different upholstery and style. (Photo: Sherrill Furniture)
Pittmon has also used Leo in a scan-to-CAD capacity with SOLIDWORKS, to reverse engineer furniture. One such project involved a classic chair that had no design drawings to accompany it. Less than a day later, and the Sherrill Furniture manufacturing team can now reproduce it anytime in a range of variations, on demand.
Reverse engineering with Artec Leo: CGI renders of the original classic chair (L) and the final customized version (R). (Photo: Sherrill Furniture)
Explaining this project, Pittmon said, “If you take a look at these two chairs, the one on the right doesn’t even exist. From the Leo scans, the CGI team created a 3D model, extending the back higher. They can also stretch out the width of the chair into a love seat or even a complete sofa.”
Artec Leo scan of the original classic chair, in Artec Studio software. (Photo: Sherrill Furniture)
He continued, “These customized versions of the chair don’t need to be physically created right now. We’re building them virtually. And then, later on, manufacturing can respond to that need.”
Whenever design drawings don’t exist for a piece, Pittmon can quickly construct a CAD model of the virtual chair or sofa using SOLIDWORKS and send it on directly to the product development team at the furniture factory.
Design drawings for the customized version of the chair, created by the Sherrill Furniture CGI team. (Photo: Sherrill Furniture)
Finding new solutions
Allen spoke about the contrast between old and new: “Early on, we conducted a side-by-side comparison of traditional photography vs our new 3D CGI pipeline with Leo,” he said. While the 3D approach does initially cost more and take longer to complete overall, it does allow them to leverage the 3D model with multiple fabrics, finishes, and more.
“[Using 3D scanning] is at least 30X more efficient on a cost-per-visual-asset basis than traditional photography. And, we’ve actually improved the visual quality vs photography,” he continued. “It’s an amazing result.”
CGI-rendered 3D models of the original classic chair (L) and the customized version with extended back (R), from Artec Leo scans. (Photo: Sherrill Furniture)
He added, “An example of this came up during the testing, when our team realized that a sofa hadn’t been photographed. The photography team had to cancel the shoot and make plans to re-shoot in 4 weeks when the sofa would be ready.”
“In contrast, the CGI team took the 3D model of the chair that was made from Leo scans, matched the sofa frame to it, and used that to digitally create 100% accurate visuals for the sofa in a 2-hour window from start to finish.”
Allen and his team continue to refine their workflow as they look for any edge that will further accelerate the pipeline while never sacrificing even a millimeter on quality.
Product: DMP Industry: Automotive and Transportation
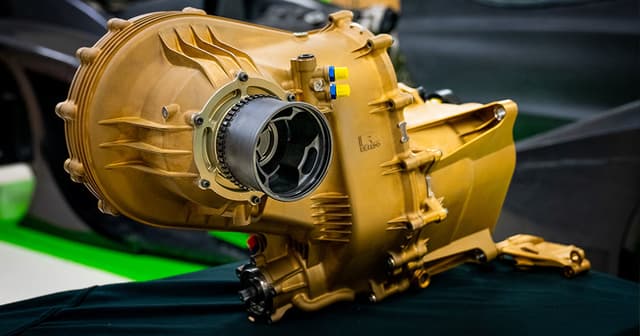
Rodin Cars, a New Zealand-based car manufacturer, is using 3D Systems’ large-scale DMP Factory 500 metal 3D printer to produce the titanium components of its new bespoke track car, the Rodin FZERO. With performance and quality leading every engineering decision, the car is manufactured primarily from carbon fiber and titanium. 3D Systems’ metal additive manufacturing (AM) was selected as the production method for all complex titanium components to enable Rodin Cars to advance the design and performance of every part, regardless of size, including the eight-speed sequential gearbox – an industry first.
“Our goal was to make every component of this car the best that it can be. The Rodin FZERO can only be manufactured with additive manufacturing.”
Adam Waterhouse, Lead Engineer, Rodin Cars
Rodin Cars’ top priorities were to optimize for weight and function while using a non-corrosive material to maintain peak performance and appearance over time.
ACHIEVING LARGE-SCALE HIGH QUALITY TITANIUM PRINTED PARTS
Targeting a final weight of only 650 kilograms and producing 4,000 kilograms of downforce, the single seat Rodin FZERO (for “zero restrictions”) is engineered to lap a circuit faster than a current Grand Prix Formula One racer. With industry-changing engineering built into every component, Rodin Cars was intent on thorough optimization to deliver the ultimate component for every part.
When it came to using titanium additive manufacturing throughout the car, challenges arose as part sizes increased – particularly for large parts. Producing components like the gearbox to spec required a build volume beyond the capabilities of most metal printers. However, reverting to conventional methods of casting the gearbox in magnesium was not an option, as both the method and material would fall short of Rodin Cars’ objectives. To deliver the ultimate hypercar, Rodin Cars’ top priorities were to optimize for weight and function with AM, and use titanium for its value as a premium, non-corrosive material that will maintain peak performance and appearance over time.
Innovation to Create a Lightweight Gearbox
The first step in optimizing the gearbox was creating a custom design together with renowned gearbox manufacturer, Ricardo. Following extensive work with 3D Systems after first adopting AM, Rodin Cars shared its gained knowledge with Ricardo, educating them on the unique benefits and capabilities of designing and manufacturing with additive. Rodin Cars needed very specific gear ratios and case dimensions, and knew it could only produce its design using AM. Removing excess mass was also a top priority, yielding thin walls down to 2mm thick in some areas. The two companies collaborated to design parts around the optimized geometry Rodin Cars was after, integrating internal galleries and fluid channels to help reduce the footprint of the final gearbox, which measures 400mm x 650mm x 300mm.
To produce titanium AM parts with the required dimensions and accurate features, Rodin Cars selected 3D Systems’ direct metal printing (DMP) for its unique large-format capability and proven quality and repeatability.
The DMP Factory 500 delivers exceptionally strong and accurate parts with high chemical purity, and the repeatability needed for serial production.
Proven Titanium Workflow
Optimizing the power to weight ratio is critical for high performance vehicles. As such, the ability to print the complex metal components in titanium was key for Rodin Cars’ mission to deliver premium performance while taking out as much weight as possible throughout the car. The integrity of titanium as a non-corrosive material also means neither the looks nor performance will degrade over time, which was important to Rodin Cars founder, David Dicker.
According to Adam Waterhouse, lead engineer at Rodin Cars, effectively any component that is metal and isn’t a bolt is 3D printed. “Every bracket through to the gearbox has been printed,” said Waterhouse. “It’s an enormous range of parts. It’s very much a printed system.” The final titanium gearbox is printed in LaserForm Ti Gr23 (A), and weighs only 68 kilograms, including steel internals.
3D Systems’ complete metal solution includes 3DXpert software, an all-in-one software for preparing, optimizing, and managing the metal printing workflow. For each of 3D Systems’ LaserForm materials, this software includes extensively developed print parameters, packaging the expertise of 3D Systems’ engineers within the workflow. The unique system architecture of 3D Systems’ DMP machines is also designed to enable full material usage without degradation.
The DMP Factory 500 is the only available scalable metal additive manufacturing solution capable of producing high quality seamless large parts of up to 500 mm x 500 mm x 500 mm.
Large Scale Metal 3D Printing
Rodin Cars initially planned to split the gearbox into multiple smaller components and print them in-house using their legacy ProX DMP 320 machines. To spare them this extra effort, the engineering team was excited to learn about 3D Systems’ DMP Factory 500, the only available scalable metal additive manufacturing solution capable of producing high quality seamless large parts of up to 500 mm x 500 mm x 500 mm. Using this new platform, the gearbox can be produced as an assembly of only four sections that can be produced in a single build.
The DMP Factory 500 features best-in-class oxygen levels (<25 ppm) and an inert printing atmosphere to ensure exceptionally strong and accurate parts with high chemical purity, and the repeatability needed for serial production. According to Waterhouse, this quality was put to the test with the thinly-walled cases of the gearbox, measuring just two millimeters thick.
“These prints were proven to be extremely accurate,” said Waterhouse. “On our largest section, which is enormous, there was only 0.2-degrees twist in the part, which is really impressive. Not to mention, we have all the benefits of additive with the internal channels and incredibly thin walls that would be impossible to achieve any other way.”
Metal Expertise from Application Innovation Group
To expedite access to large-scale metal printing in advance of the installation of its own DMP Factory 500, Rodin Cars worked with 3D Systems’ Application Innovation Group (AIG) to get the first titanium gearbox printed. 3D Systems’ AIG is a global resource equipped with the experience and technology to support AM applications across industries, and can advise and assist on projects at any stage, from application development and frontend engineering, to equipment validation, process validation, and part qualification.
3D Systems has provided Rodin Cars with ongoing knowledge and technology transfer since it first adopted additive manufacturing, helping the car company to increase its understanding of necessary principles for success with AM design and production. However, the shift to a large-scale printing format required a new set of best practices. 3D Systems’ AIG provided engineering and application development services to help Rodin Cars prove its concept, including final programming of the four gearbox components and printing of the first gearbox. 3D Systems also provided the programmed build files and technology transfer to accelerate Rodin Cars’ path to successful large-scale metal printing following the installation of the DMP Factory 500 at Rodin Cars’ facility.
Product: Solid Edge Industry: Automotive and Transportation
Developing fresh, disruptive solutions for automotive and motorsport
In 2017, Ashley Warne, chief executive officer (CEO) and chief engineer of Dynisma Ltd., founded the United Kingdom-based driving simulator company after leading the in-house simulator development efforts for F1 at both McLaren and Ferrari. “Working in high pressure, excellence-led teams with significant resources instilled the belief that these efforts could be applied differently,” says Warne. “Access to the most advanced, high-fidelity, responsive motion generators that engineers could want should be made available to all.” At Dynisma, Warne is responsible for technical leadership and developing simulation concepts.
“Dynisma produces the most dynamic, responsive and scalable driving simulators in the world. Our team of world class engineers have taken on a fresh perspective and invented new solutions for automotive and motorsport,” states Warne.
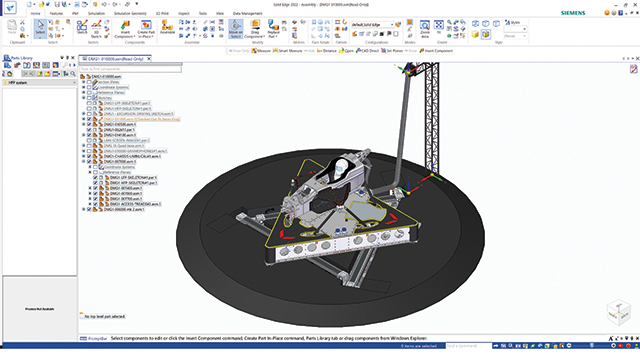
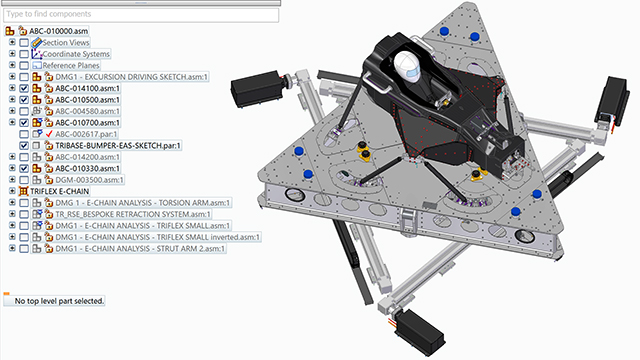
Dynisma Motion Generators (DMGs) are fully immersive, offering the perfect solution for a range of audiences, such as motorsports teams that want to optimize driving and car performance or automotive manufacturers and suppliers that need advanced vehicle development and testing. The DMG delivers maximum bandwidth with minimum latency, which means that the simulator reacts very quickly to commands – in this case, response happens in 3 to 5 milliseconds. This is possible because the team co-designs software and mechanical engineering aims to remove every possible obstacle between the driver and the data.
DMGs are produced for all use cases in driving simulation for automotive and motorsport. The simulator also includes visuals, mock-up chassis, vehicle models and environment simulation. “DMGs are at least 50 percent better than any other comparable solution in the world and equally affordable,” states Warne.
Designing the DMG
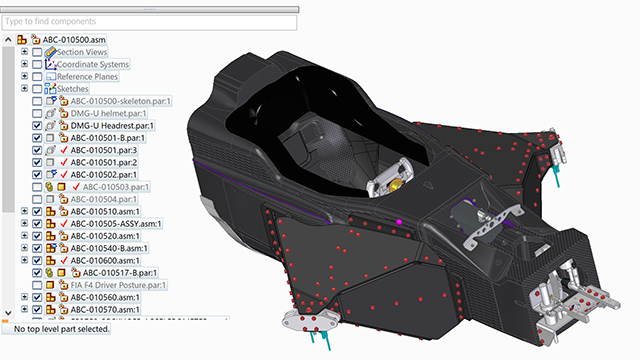
“The development of DMGs always starts with embodying our unique selling points,” explains Matt Bell, head of mechanical engineering at Dynisma. “The process begins with a conceptual state, which gives the team a broad layout of the system before it is handed over to mechanical engineering. Then we identify and set all the key dimensions and components that will comprise the DMG. Once we feel like we have that arrangement correct, we tend to spread the work out to the rest of the team who will detail, draw and transform it into something that is producible. We also work with various suppliers who manufacture the structural parts – whether it is through formed metal work, computer numerical control (CNC) machined and 3D-printed components, or a composite structure.” Once the team figures this out, they have subassemblies or components come in for assembly and test.
“All our systems have very low latency,” summarizes Warne. “When we want a driver to feel that they are being moved – for example, from oversteer – this will happen in 3 to 5 milliseconds.” DMGs can be used to simulate any event like road texture, rumble strips, oversteer feedback and noise, vibration and harshness (NVH). Delays of milliseconds can have a huge impact in terms of the feedback given to the driver and their response.
Overcoming challenges as a startup
Like any startup, Warne and his team found the process of getting a business off the ground to be a challenging endeavor. “One critical success criterion is probably how fast you can bring your solution to the market,” Warne reflects. “That’s why we were looking right at the beginning for affordable yet advanced software to fulfil our needs in the mechanical design process of modeling and drafting, as well as a system level structural simulation solution.
After studying what was available on the market, Dynisma turned to Siemens Digital Industries Software and its Solid Edge for Startups program, which provides eligible startups with free access to a complete portfolio of product development software tools.
Along with one year of free Solid Edge® software, the program provides access to training resources, best practices and guidance from experts.
“When you are a fresh business with fresh investor funding, one of your primary focuses is making the capital you raise go as far as possible. So, the Solid Edge for Startups program was quite attractive at that time,” explains Warne. “It gave us this runway with a fixed cost for a certain amount of time, which provided flexibility in terms of licensing and enabled us to scale up as we took on new designers.”
As Dynisma applied for the Solid Edge for Startups program, they found the process to be painless. “We were able to quickly get the software licenses in place and integrate it with our cloud-based file sharing. From here, it was easy to get people up and working,” explains Bell. “When we were testing competitor options, some were more difficult to get and didn’t work properly a month in. With Siemens’ solution, the ease of setup and integration was a big influence on our decision.” By using Solid Edge, Dynisma’s onboarding licensing support process is now significantly faster compared to competitors. They can be up and running in days versus months.
Excellent support and advanced features
“The Solid Edge for Startups program was appealing because it offers the full digitalization portfolio covering mechanical and electrical needs with high quality technical support,” states Warne.
Dynisma has found Solid Edge to be the most useful for producing 3D models, rendering, drafting, simulation and for its built-in data management functionality, which enables them to manage new and existing files. The integration between applications allows Dynisma to significantly increase efficiency in their workflow. “The built-in data management system is a useful element that is not available in some other software packages,” states Bell. “We found the sheet metal modelling capabilities of Solid Edge to be excellent. It’s both powerful and user friendly enabling our new starts to quickly get productive with minimal rework.” Also, the assembly instructions are produced in Solid Edge. The team builds up the machine and moves through their verification and validation (V&V) activities and factory acceptance testing.
Siemens solution partners IC Blue and OnePLM also offered valuable support, making sure Dynisma got set up with licenses and received technology support during the implementation. Since then they have provided technical support and training for new team members at Dynisma. The quality of available technical support was one of the key reasons why the team chose the Siemens’ solution. “It was easy to get fast and reliable support from skilled people who could answer any question,” explains Bell.
Additionally, although Dynisma has scaled up and become more autonomous, they still benefit from the technical support, which enables them to discover and explore additional capabilities included in the software so they can become more proficient. “If we are experiencing an issue, the technical support team will set up an educational session and enable us to better understand how to overcome a problem,” states Bell.
Getting up to speed in days
The ease of onboarding and using Solid Edge has enabled Dynisma to rapidly bring team members up to speed and ultimately help them grow. “One way Solid Edge enables us to meet our design goals is that it is easy to pick up,” Bell explains. “We can find people who have used other Siemens packages, like NX, and they can quickly find their way around Solid Edge. Additionally, we have had several people come in who have used different packages who can pick up the software in a few days and produce useful work. This helps because it enables us to be responsive.
“It is now very easy to produce offers quickly, which also helped speed up our design and delivery processes – in the end the whole customer experience benefited from that shift.”
Going from startup to scaleup with Siemens Mechanical Design software
After the end of their startup phase, Dynisma expanded their product development capabilities to a new level by implementing Siemens Mechanical Design, which includes access to capabilities from both Solid Edge software and NX™. “Choosing this solution can enable us to grow while still being flexible enough to set the focus we want,” reports Bell. “After having an excellent experience with Solid Edge, the step to Siemens Mechanical Design was logical. It makes it easier to transfer in and out with NX files, improving interoperability with other software.”
The Siemens Mechanical Design software, including Solid Edge software and NX software, are part of the Siemens Xcelerator portfolio, the comprehensive and integrated portfolio of software, hardware and services.
The package itself provides a single source for all mechanical computer-aided design (MCAD) purchasing, licensing, training and service needs. “For us the main advantage of Siemens Mechanical Design besides agile licensing was to provide each designer or engineer with the features and functions needed for the specific development process they were assigned to. This was to maximize design capabilities while lowering total cost of ownership,” says Bell.
It is crucial for Dynisma to continuously produce conceptual models and develop detailed designs with them. Since it is a highly integrated package, they can do so. Along with the ability to pick it up quickly, there is a flexible licensing model where they can pay by the month in the case of a short-term contractor.
“As we grow, we plan on continuing to explore Siemens Mechanical Design, moving toward using more capabilities with the hybrid licenses,” states Bell. Looking further down the road, they will continue to broaden access to their groundbreaking technology, offering industry leading responsiveness in new sectors and markets.
Product: Figure 4 Industry: Automotive and Transportation
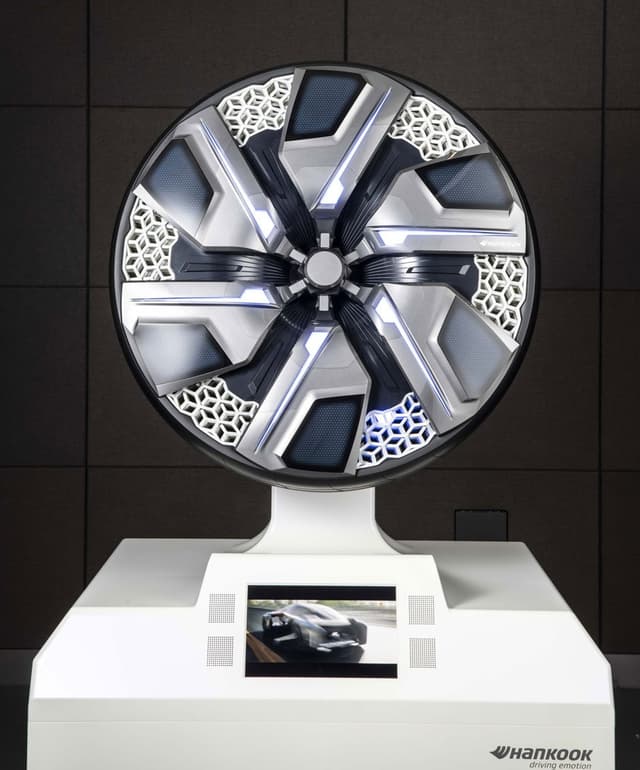
Hankook Tire & Technology is more than a tire manufacturer. With a focus on automation and technology that will enable “The Future Driving Innovator,” the Seoul-based company has put electrical vehicles at the center of what they do. Recently, Hankook needed a way to quickly and cost-effectively drive innovation by iterating multiple plastic and elastomeric designs with complex geometries for its i-Flex nonpneumatic tire (NPT), which would eventually become a key component in Hankook’s award-winning HPS-Cell autonomous mobility platform. By leveraging 3D Systems’ plastic and elastomer additive manufacturing technologies, Hankook’s Design Studio was able to quickly iterate designs and share production-grade parts among their designing, and testing teams while reducing costs.
“The main purpose of using 3D printing is to communicate better with R&D before they build the actual mold to produce the tire. The traditional molds are machined and cost a lot of money and time to develop, but that’s also been the conventional way to figure out a new design, shape, and even volume. Now, using additive manufacturing technologies from 3D Systems, we can work faster with R&D to figure out the shape or structure using small portions of the structure and then test our prototypes for safety, noise, and other parameters.”
– Rosa Youn, Design Innovation Studio Manager, Hankook Tire & Technology
The Challenge
Expedite multimaterial, complex tire and wheel designs and testing while cutting costs
Hankook Tire & Technology understands that autonomous mobility solutions of the future require a new generation of tires that combine minimal maintenance with maximum safety and comfort. With their low maintenance and increased safety, NPTs are predestined for this field of application but developing an NPT that checks all these boxes presented a complex and costly design challenge. Hankook designers believed that a biomimetic design that mimicked biological tissues would provide internal support for the NPT, but with a nearly infinite number of possible cellular structure designs, Hankook’s Design Studio needed a way to quickly evaluate partial parts as well as scale complete models.
Traditional prototyping methods for new tires often started with a 2D sketch, transitioning to a 3D CAD design that would be translated into an aluminum mold through skilled human machinists. The entire process was too costly and too slow, with each iteration taking potentially weeks or months.
Furthermore, the NPT’s biomimetic supporting “spokes” matrix challenged even the most capable machining stations due to its complex hollow, interconnected structures. After exploring multiple additive systems for rapid prototyping and low-volume production, Hankook chose 3D Systems’ Figure 4 technology platform for the plastic support structures and rubber tread. Hankook also turned to 3D Systems’ partner CP Tech for selective laser sintering (SLS) for conepting the metal tire structures and hinges, which turbocharged the development of their i-Flex NPT prototypes. The result, as Hankook designers like to say, is the future of mobility.
The Solution
1 – Spoke Structures for Nonpneumatic Tire i-Flex
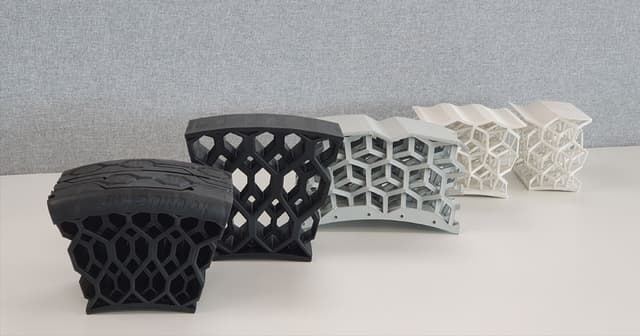
Various iterations and concepts of spokes printed with 3D Systems additive manufacturing technologies (r) that led to the final design of the Hankook HPS Cell (L)
Hankook’s NPT tire includes a complex biomimetic plastic matrix for internal support, an elastomeric external tire tread, and metal parts that perform some of the support functions of a tire rim plus additional functions necessary for autonomous vehicles. Machining these hollow structures in plastic would be nearly impossible.
“For us, because of [3D Systems’] additive manufacturing technologies, we can design or make anything we want to or anything we can imagine. This technology can eliminate the limits of manufacturing, which is really great for us. With traditional product design for example, building and machining, there are a lot of limits. Machine tools have limits. Additive manufacturing does not have these limits,” said Hee Sung Jang, Design Innovation Studio Designer, Hankook Tire & Technology.
Using the Figure 4 platform, Hankook designers are able to quickly iterate different support matrices using Figure 4 PRO-BLK 10 plastic with its thermoplastic-like mechanical properties. The Hankook Design Studio team could quickly turn 3D designs of different biomimetic matrixes into partial or scaled prototypes that maintain the same cellular spacing ¬— which is critically important to downstream testing — all while constraining development costs. With partial parts that include full-scale cellular structures, Design Studio designers could quickly gauge relative strengths among candidate designs using physical testing before proceeding into full tire assembly.
2 – Noise Control Testing on Tire Segments
Tires, including NPT tires, need to be safe and durable, but they also need to be aesthetically and acoustically pleasing. In short, people won’t buy ugly tires, and they won’t keep buying loud tires. After developing the NPT support matrix, Hankook Design Studio designers were able to develop partial and scaled tread designs using Figure 4 RUBBER-65A BLK elastomeric materials.
“By using those materials and partial parts, we can evaluate the part for noise and safety,” said Mrs. Youn. “The test system flows air or water into the channel or groove, [and] we measure the noise to understand if the structure is correct or not.” She added that in the future, building these treads in translucent Figure 4 material will make the process even easier, allowing engineers to see how fluid travels down the tread grooves, a key part of tire safety in adverse weather.
Additionally, printing tire treads makes it easy for manufacturing engineers to evaluate new NPTs for stability and potential cracking and reduced reliability.
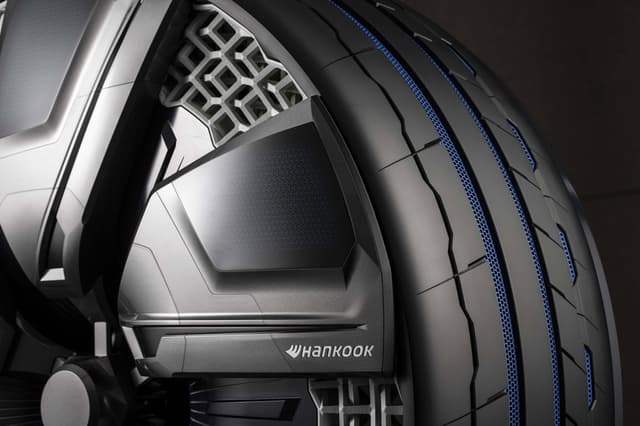
Hankook’s NPT design includes plastic components for internal support, rubber materials for tire tread, and metal components for tire rim and support. All three elements are shown here.
3 – Moving Parts on New Concept–Type Tires
Additive manufacturing’s ability to develop complex shapes also allowed Hankook designers to develop internal grooves and structures that help connect the tires’ three primary elements: tread, NPT support matrixes, and moving thermoplastic rim components. The thermoplastic components were manufactured by CP Tech, using 3D Systems’ SLS technology. This was new to Hankook, as traditional tires don’t consist of any moving parts.
“One of the main reasons we chose 3D Systems over the competition is that their material selection is so broad,” said Rosa Youn, Design Innovation Studio Manager, Hankook Tires. “It covers all the material requirements we have. In addition the Figure 4 is fast. Time saving, reliability, service, best troubleshooting, and also availability of the system and reasonable price were our key decision factors. We believe in the value of 3D Systems’ Figure 4. For me it is one of the best additive manufacturing systems in the world.”
4 – Standard Visual Prototypes of Tire Profiles
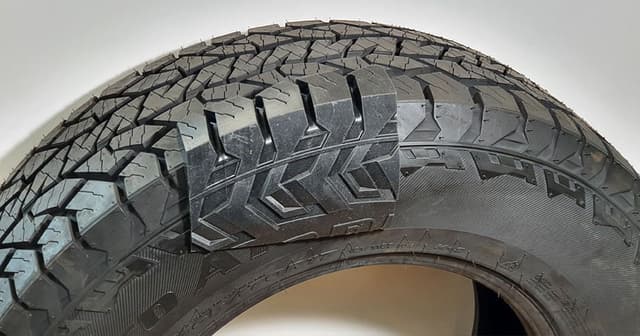
Hankook Design Studio has already expanded the use of the Figure 4 platform, using it to develop traditional tire treads and profiles for testing. This is allowing for faster iterations of all new product designs, not just the revolutionary but the evolutionary as well.
In addition to helping Hankook’s Design Center quickly develop and test NPT tire designs, the company can also use it to quickly evaluate new tread designs for road noise and other key factors, reducing time to market and costs for all new tire designs at Hankook.
In addition to helping Hankook’s Design Center quickly develop and test NPT tire designs, the company can also use it to quickly evaluate new tread designs for road noise and other key factors, reducing time to market and costs for all new tire designs at Hankook.
Product: Solid Edge Industry: Automotive and Transportation
Supporting the electric mobility ecosystem
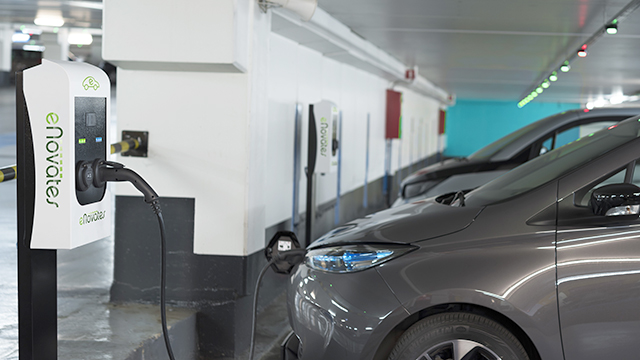
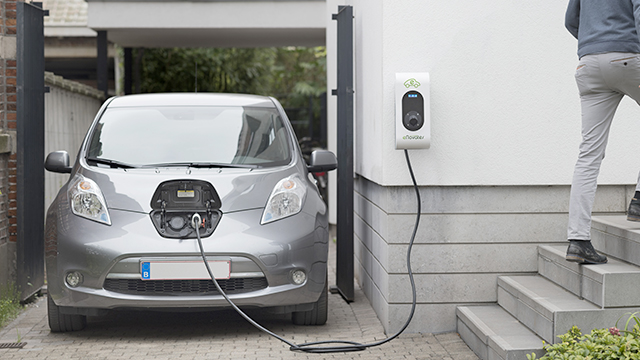
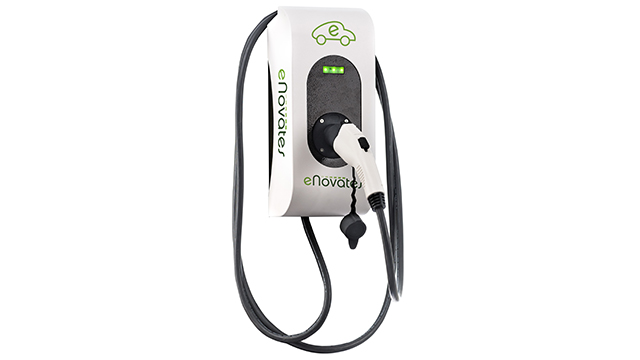
eNovates is a rapidly growing technology company driven by mobility and sustainability. The company was founded in 2010 as a think-tank in a business club focused on developing and producing charging systems and energy management software to support the electric mobility ecosystem.
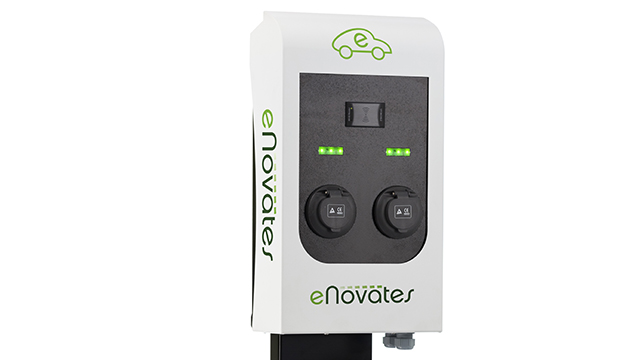
eNovates is expanding in the European Union and has an important market share in delivering public charging infrastructure, with about 80,000 charging stations installed in early 2021. The company is expanding its reach into smart energy management and recently added a vehicle-to-grid (V2G) charger to its portfolio. Its customers are charge point operators (CPOs) – companies who sell charge points, connect them to networks and provide maintenance. eNovates serves its CPO partners as an original equipment manufacturer (OEM).
“Some of our customers approach us with no more than an idea for the final product. In this case we can base ourselves on a set of generic platform components and products to realize the best-fit custom product for the customer,” explains Stijn Vispoel, research and development (R&D) manager at eNovates. “Others come to us with an enclosure and ask us to develop a charger for it. We do full projects for them, and all solutions include mechanical, electrical, electronic and software components.”
Product development for rapidly changing requirements
Technologies, regulations, standards and customer requirements are evolving quickly in the electric mobility ecosystem. “The biggest challenge is the constantly and rapidly changing guidelines in the market,” Vispoel says. “We have to be on top of all the new developments and we really need a new product every year. It’s important to have enough R&D capacity to keep up with the changing requirements for charge points. Another factor is the different regulations in different countries in Europe. For example, customers in the Netherlands have different requirements than customers in France.”
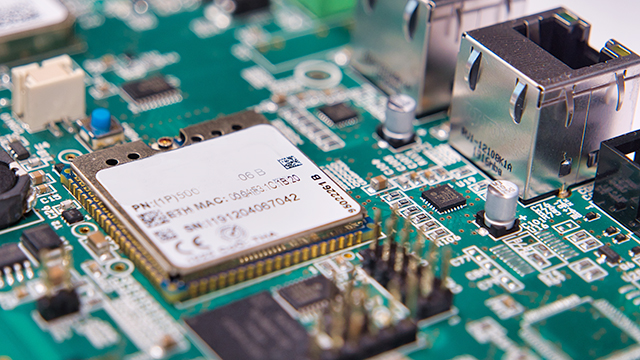
Vispoel leads a team of project managers and support personnel with varying back-grounds in mechanical, electrical and electronic engineering. “We begin each project with a prototyping phase where we develop the printed circuit boards we need, the electrical wiring and mechanical components,” Vispoel explains. “Once we do all the checks on the digital design files, we make some prototypes and do test runs to confirm that they comply with the customer requirements and regulations. Then we enter what we call the alpha phase, redesigning any components that need modifications. We make another batch of the product, around 30 to 50 chargers, and do another validation run, performing temperature and high-voltage tests. We also have customers who use them to charge cars and run additional tests.”
In the next stage of development, the beta phase, eNovates makes necessary design modifications and orders a new batch of the product. “We go directly to certification labs with the beta chargers, and place about 100 chargers in the field with our customers, so we are certain that the product is mature enough and it’s fully certified to go into the market,” says Vispoel. “At that stage we typically don’t develop the hardware further – the focus is on finishing the software. Finally we go into production for our customers.”
Disparate systems and information silos
Over its history, eNovates had acquired engineering software systems for mechanical computer-aided design (MCAD), two different printed circuit board (PCB) design solutions, and a system for electrical wiring and harness design. The systems had been selected based on engineers’ prior experience and partners’ and customers’ use of the solutions.
This software landscape had some limitations: The MCAD system lacked electrical design functionality, the wire harness design system had no 3D capabilities and neither system easily exchanged data with the PCB design tools. The four separate and disconnected software solutions created information silos that hampered interdisciplinary collaboration. Each software package used different data formats that impeded transfer of information between disciplines. Because the software was purchased from different vendors, the new versions of each software solution were not synchronized with the others and eNovates had four different sources of support.
Using this approach, the mechanical design team sent their design models to the electrical team, which amended the designs and returned them to the mechanical team. These iterative design exchanges continued over weeks and months, resulting in huge design and prototyping costs and product launch delays. The information silos and barriers between systems made it difficult for eNovates to fit electrical designs into mechanical spaces. They also created problems in communicating design information to contract manufacturers. eNovates was sending confusing and disconnected details of the design for manufacturing, which resulted in issues with requirements and regulations.
Integrating engineering disciplines and solutions
To eliminate the workflow inefficiencies, eNovates searched for an integrated software toolset that better suited the fast pace of development. From contacts at Ghent University, the eNovates team was introduced to Solid Edge® software, which is a part of the Xcelerator™ portfolio of solutions and services from Siemens Digital Industries Software and a leading mainstream product development platform.
eNovates contacted ADOPT id PLM, a Siemens solution partner in Belgium. After an initial meeting, ADOPT id prepared a presentation for eNovates that included Solid Edge and its integrated electrical design and technical publishing tools. The demonstration illustrated how all of the Solid Edge mechanical design, electrical wire routing and harness design, and technical publishing applications were fully integrated and used the same data format and user interface conventions. ADOPT id also proposed Siemens EDA (formerly Mentor) PADS Professional software, also integrated with Solid Edge, for PCB design and verification (PADS is supported by Siemens EDA solution partner Innofour). The presentation also emphasized the bidirectional data flows and associativity across the mechanical, electrical and electronics domains – design modifications in each discipline are automatically reflected in the others.
eNovates quickly made the decision to choose the proposed Siemens solution for several reasons. “We wanted all of our software tools to work together so we could have a streamlined design flow for our fastpaced development,” Vispoel explains. “For complex products with high quality standards and efficient production, we needed to transfer information very efficiently. The Siemens software offered us a better match to help us make fewer errors in our design iterations. We didn’t find this level of integration anywhere else in the engineering software market. And we regard Siemens as a very big technology provider, a market leader in software and a brand that delivers quality.”
Documenting designs for manufacturing
“We fully outsource our production,” Vispoel says. “We deliver the contract manufacturer a full package of information on how the product has to be made, how to test it, how to package it. And then they translate what we do in engineering into making the product. They source every component, make every PCB and test everything based on the instructions we provide.”
With its previous software solutions, eNovates could deliver a 3D file depicting the mechanical design, electrical drawings, and three separate bills of materials (BOMs) for drawing mechanical, electrical and PCB content. However, the information was not well integrated, and its delivery was not efficient.
Solid Edge Technical Publishing software offered eNovates a superior solution for preparing information for manufacturing. Now, the manufacturing package includes a unified BOM for the entire product, which is especially useful for pricing. For PCB manufacturing, a standard format file produced using PADS Professional software includes information about each physical board layer and coordinates for PCB objects like copper traces, vias, pads and solder masks. For electrical manufacturing, Solid Edge Technical Publishing software extracts the list of cables and their locations, connections, cut lengths, and torques required on their connecting screws, all produced using the Solid Edge electrical design software. With the Solid Edge 3D model, the publishing software fully and visually describes each step in the product assembly and testing processes.
Streamlined workflows boost efficiency
With the new integrated toolset, eNovates benefits from improved efficiency throughout the development and manufacturing cycle. “This was a big win for us,” Vispoel says.
Solid Edge 3D design software includes synchronous technology, which enables eNovates to edit CAD data from any source and leverages built-in product data management and cloud collaboration tools. Solid Edge electrical design satisfies eNovates’ need for 3D wiring and harness design and validation in mechanical assemblies.
Solid Edge technical publishing has helped eNovates improve the clarity, accuracy and completeness of manufacturing information in comprehensive case files. The integration of PADS Professional with Solid Edge has helped improved communication between PCB designers and mechanical engineers.
Product: HandySCAN Industry: Automotive and Transportation
How Hyundai Design North America uses HandySCAN 3D for improving real-time design workflows
Opened in January 2003 and located in Irvine, California, Hyundai Design North America’s design and technical center is a 90,000 square foot, $30 million state-of-the-art facility where automobile designers, engineers, model makers and other experts create new vehicles. The team offers alternative designs for its parent company based in South Korea.
As is the case with the vast majority of automotive manufacturers, clay sculpting plays a vital role in the design process in Hyundai Design North America’s studios in order to fine-tune concepts based on scale models and full-size clay vehicles. Clay modelling to design vehicles is still a very common practice with today’s automotive manufacturers to assess design quality and get feedback from reflection-based surfacing.
However, with today’s amplified competition for consumers as well as manufacturers’ accelerated time-to-market development and production schedules, design teams are under increasing pressure to create concepts faster than ever before. Digital modeling using 3D measurement technologies, such as portable 3D scanners, has become a vital solution in order to speed up design workflows.
Legacy 3D scanners no longer fitted the performance bill
For a long time, Hyundai Design North America, which is an early adopter of new technologies, used 3D scanners as a complement to its clay modeling and design processes. Unfortunately, at one point, the team realized it was time for a major equipment upgrade.
“The scanners that we were previously using were too bulky and difficult to manage. The scanning process and post-processing times were long and required most modelers to step away from working on the clay,” explained Rob Homer, Operations Modeling Manager at Hyundai Design North America. “This led to crucial time loss, especially when deliverables had hard target dates.”
Rob and his team began checking out available 3D scanners that fit their requirements. “We wanted a 3D scanner that was compact, easily portable, fast and accurate. It also had to be compatible with our CAD software.”
HandySCAN 3D: A clear front-runner in 3D scanning for designing vehicles in the automotive industry
“After looking into the various 3D measurement technologies out there, Creaform came on top for me with its HandySCAN 3D. It is a very good and reliable product at a very good price point,” Rob added. He was equally impressed with its ease of use and speed.
Hyundai Design North America was able to seamlessly implement HandySCAN 3D into its existing design workflows for real-time development. Training users on the software was completed in a day. “The experience from purchasing the scanner to training was incredibly pleasant and professional.”
Once the 2D sketch is settled, digital modelers get to work on the 3D clay models and mill it out for verifications and fine-tuning. Changes are performed by hand on the clay model, which is then 3D scanned to acquire the digital representation of the modifications.
“The scanning process is quick and easy. We are able to scan selected areas of the model without disturbing anyone working around it,” he said. “We can relay information to the digital team within minutes after finishing the scan.” This quick turnaround time of the scan data to the digital modeler means that affected areas can be fixed quickly to mill the model again before final reviews.
Richard Gillespie, Senior Digital Modeling Manager, says that the 3D measurements enable the modelers and design team to know exactly where the clay models are landed in comparison with design criteria and styling boundaries. They can quickly identify and correct discrepancies. Designers can come to decisions faster thanks to the efficiency and accuracy HandySCAN 3D offers.
One of Rob’s favourite aspects is HandySCAN 3D’s simplicity. “My modeling team can use it independently without having to wait for another expert to do the scans for them. That makes our services a true one stop shop.”
Hyundai Design North America will continue to improve their clay modeling workflows using 3D scanning in order to allow more time for the design process and refinement. We look forward to seeing the new designs hit the market!
Product: NX, Simcenter Industry: Automotive and Transportation
The rise of Scuderia AlphaTauri
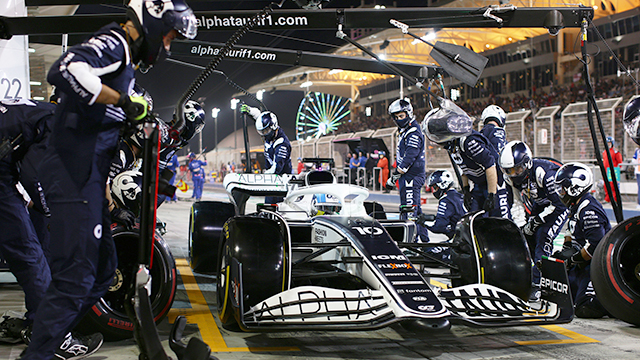
On February 23, 2022, the world got a taste of the new Formula One (F1) cars as they completed their pre-season test days in Barcelona. This was followed by testing days in Bahrain in early March 2022, where the drivers focused on getting comfortable driving the new cars before the race season began on March 21, 2022.
During the test days and the first few races, two young Scuderia AlphaTauri drivers, Pierre Gasly and Yuki Tsunoda, worked with the Scuderia AlphaTauri engineers to discover how the new car performed and fix the mistakes that occurred with the new design.
“There are new things to discover with this car every time we go out on the track so we have to make the most of each session and learn as much as we can before the first race here,” says Pierre Gasly, trackside during the test days in Bahrain in March 2022. “The feeling was unique. I was excited to discover these new cars and see how they felt on the track.”
That feel-on-the-track performance enhancer
In F1 racing, the driver and the car become one. This feel on the track comes from the part of the car that normally doesn’t get to be in the spotlight, the driver’s seat.
“The chassis is one of the most sophisticated parts of the car for safety and performance reasons. You need to start working on that part immediately even if you don’t have all of the information,” says Raffaele Boschetti, head of information technology (IT) and innovation for Scuderia AlphaTauri. “Before partnering with Siemens, we spent three months producing a good chassis. With Siemens software, we did this in one month. This saved us a lot of time and gave us many advantages.”
Aside from the chassis, the seat is important for driver safety and overall driver performance. Overall seat design is strictly regulated by F1 safety and crash test rules. If something goes wrong, drivers need to be able to exit the car quickly and safely. The safety marshal and medical teams need to be able to extract injured drivers from a crash effectively. Boschetti is quick to point out that there is much more to the seat in an F1 car than just safety.
“The seat is a part of the car that delivers performance. The driver feels all of the vibrations, accelerations and handling through the seat. On the track, we can modify the car settings to improve the car based on the driver’s needs,” says Boschetti. “In Formula One, you have a couple of tests in February or March. In this situation, the software and platforms Siemens provided us were vital to building the seat.”
One size does not fit all
Not every F1 seat is the same. Composite design engineers will tell you that half of the challenge isn’t the seat but how to fit the driver in the car.
“It is like a tailored suit. You have to look at things in terms of helmet position, back position and you have to be as low as possible,” says Francesco Dario Picierro, senior composite design engineer for Scuderia AlphaTauri.
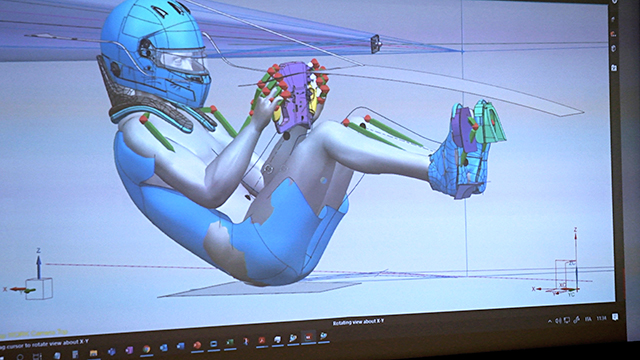
To ensure these critical performance aspects were correct, Picierro and his colleagues developed a unique seat-designing process. To start, they designed a slightly larger seat than necessary and then heated a batch of special resin and took a physical mold of the driver’s body in the ideal position. From the resin mold, they used NX™ software to create a complete scan to design the seat. NX, the Fibersim™ portfolio and Simcenter™ software are part of the Xcelerator portfolio, the comprehensive and integrated portfolio of software and services from Siemens Digital Industries Software.
“The process might seem simple, but thanks to Siemens’ products it becomes smarter,” adds Picierro.
Using digitalization for F1 success
With the complete design and chassis change in the 2022 model, the team had to simulate every detail in computer-aided design (CAD) from overall visibility to how the driver would fit into the chassis design.
Getting the driver to squeeze in, reach the pedals and obviously see – while considering the helmet, safety regulations and the new chassis and car design – is an engineering feat in itself. The team knows that digitalization is the only way to succeed in F1 these days. Using Siemens’ digitalization tools removed most of the grunt work from the design, engineering and production cycles.
“Using NX helped us with our digitalization efforts. For example, we can replicate the exact handwork on the steering wheel or the visibility using the driver’s camera. We can also scale the digital mannequin according to the measurements of the driver,” says Picierro.
Racing against the clock
While the composite design engineers are custom fitting the driver to the seat (a process that can happen several times per season based on the needs of individual drivers) other members of the Scuderia AlphaTauri engineering team are optimizing the new car design for driver performance in time for race day.
Aside from the tight deadline, the other challenge for every F1 engineer is weight. F1 engineering teams struggled to make the minimum driver plus car weight of 795 kilograms (kg), especially with the new safety regulations and ground effect pull. At the last minute, the teams reached a compromise to increase the weight to 798 kg.
“Of course it’s always difficult. It’s a completely new regulation. These cars are complicated and it is difficult to design everything to meet the weight limit requirements. As we can see, nearly all of the teams are overweight. We also have to consider costs. It is expensive to reduce weight. Considering the cost cap, our teams were able to come to a compromise,” says Franz Tost, team leader for Scuderia AlphaTauri.
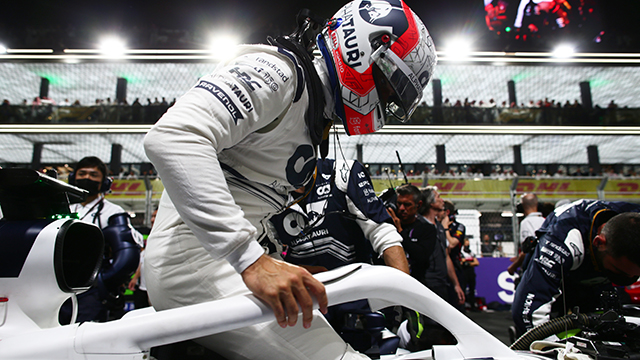
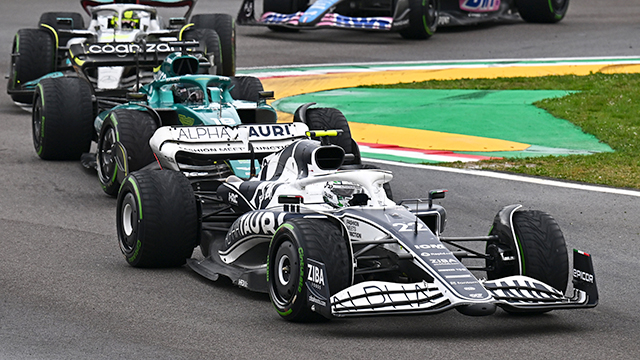
Zooming around over 300km/h during a normal F1 race, drivers experience up to four or five lateral G’s routinely under braking and cornering and during acceleration on the long stretches.
One platform and a secret to success
As Tost explained, balancing design parameters is always a challenge for engineering teams. Using the same digital platform and software suite to examine the real behavior of the car helps the team make the right decisions for the races.
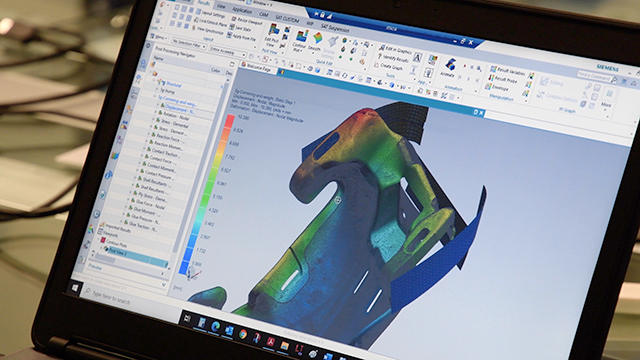
“Our job is to evaluate the strength and stiffness of the part. The driver’s seat needs to be strong enough to support the acceleration loads and stiff enough to make a proper interaction between the driver, the chassis and the rest of the car,” says Giuseppe Stiscia, a chassis group leader and structural engineer for Scuderia AlphaTauri. “We use Siemens Simcenter to generate the finite element model and generate the load model conditions.” Simcenter clearly shows the standard stiffness values of the structure via a color strip. Each color represents a state of stress or displacement of the part.
“Structural engineers use this information to understand the real behavior of the structure. Our goal is to make the part as strong and stiff as possible, but we need to optimize the weight first. He adds, “Simcenter helps us calculate the part faster and use the same platform for everyone involved in the project.”
Development time is gold
Andrea Rizzo, a research and development (R&D) digital layup group engineer, uses this same platform with his colleagues. They use Fibersim tools to finish the actual part.
“We use Fibersim to achieve a perfect connection between the FEA results and the real lamination,” says Rizzo. “With this material, you need to cut a shape in the ply to be laminated on the mold. Any extra or unnecessary material applied to the mold is an additional cost. We try to laminate with as little material as possible to save time and money.”
The Scuderia AlphaTauri engineering team also uses Fibersim to maintain the consistency of the customized parts. Unlike commercial vehicles, F1 cars contain many handmade carbon fiber parts created by carefully layering composite plies inside the laminate. Each part has unique structural characteristics. Although the team wouldn’t say for competitive reasons, one can guess that spare parts and replacement parts are created on an as needed basis.
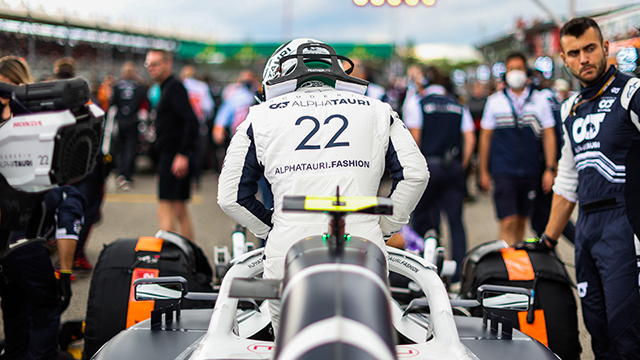
Data is king: any piece of information the team can analyze will help them understand the performance behavior of the new car.
“Each carbon part is a laminate, so we need to make sure the first one is the same as the last one. This is why we use Fibersim. We save time during the production process with this comprehensive simulation. We can prepare plies to be the same for all laminations.
“With Fibersim, we know what is happening in the component. We know the quality standard of the plies. We follow every single ply during the process. We can prevent problems before they happen because we ‘live’ in the same platform from NX to Simcenter to Fibersim. And more importantly, we save time,” says Rizzo.
“The problem with F1 especially – but even for standard cars – is that you need to produce the same part with the same quality at the same time. If you use the same suite that calculates everything for you from the CAD part to the production line, then you end up with a quality part that will deliver performance on the track. That’s the goal,” says Boschetti.
Thanks to Siemens Xcelerator tools like NX, Simcenter and Fibersim, the team can customize each seat to the driver using layers of composite plies to create a hyper-light-weight laminate that performs well to achieve safety and design specifications for the new Scuderia AlphaTauri cars. This provides Gasly and Tsunoda with the ideal connection to the car they need to perform well. Thanks to some superb engineering from the team in Faenza, Italy, and help from the Siemens Xcelerator portfolio, the Scuderia AlphaTauri team is more than ready for the upcoming F1 season.








 Zooming around over 300km/h during a normal F1 race, drivers experience up to four or five lateral G’s routinely under braking and cornering and during acceleration on the long stretches.
 Data is king: any piece of information the team can analyze will help them understand the performance behavior of the new car.